| 1 |
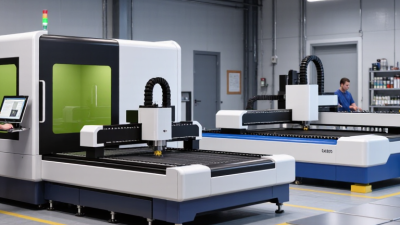
Fiber Laser Flatbed Cutter |
General fabrication, enclosures, appliances, automotive parts |
1,500 × 3,000 mm to 2,000 × 6,000 mm |
1.5–6 kW |
Mild steel: approximately 0.5–25 mm; stainless steel: approximately 0.5–12 mm |
Approximately ±0.05–0.10 mm, depending on machine and process conditions |
High speed, narrow kerf, low consumable use, suitable for automated production |
Higher initial investment; reflective metals require suitable configuration and process control |
US$80,000–250,000 |
Clean the protective window, inspect the nozzle, maintain assist-gas quality, check rails and lubrication |
Laser power, cutting head protection, chiller capacity, nesting software, service response, electrical requirements |
| 2 |
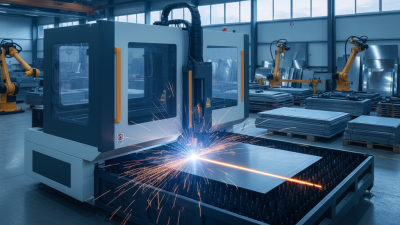
High-Power Fiber Laser Cutter |
Heavy fabrication, structural components, thick steel processing |
2,000 × 4,000 mm to 2,500 × 6,000 mm |
8–20 kW |
Mild steel: approximately 1–50 mm; actual capacity varies by material, gas, and quality target |
Approximately ±0.05–0.15 mm |
Fast processing of thick plate and high-volume orders; reduced cutting time per part |
High capital cost, greater power demand, and more demanding thermal and gas management |
US$180,000–500,000+ |
Monitor chiller temperature, inspect cutting head optics, clean the bed, verify gas pressure and beam alignment |
Factory power supply, transformer requirements, oxygen and nitrogen flow, fume extraction, foundation loading |
| 3 |
CO₂ Laser Sheet Cutter |
Existing CO₂ laser facilities, non-metallic materials, mixed-material workshops |
1,500 × 3,000 mm to 2,000 × 4,000 mm |
2–6 kW |
Mild steel: approximately 0.5–20 mm; stainless steel: approximately 0.5–10 mm |
Approximately ±0.05–0.10 mm |
Can process some non-metallic materials and may suit facilities with existing CO₂ infrastructure |
Lower electrical efficiency and more optical maintenance than modern fiber systems |
US$70,000–220,000 |
Check mirrors and lenses, maintain cooling water, inspect the laser tube, clean the beam path |
Availability of replacement optics, tube life, cooling system, ventilation, local technician capability |
| 4 |
CNC Plasma Cutting Table |
Carbon-steel plate, structural fabrication, agricultural and construction parts |
1,500 × 3,000 mm to 2,500 × 8,000 mm |
45–200 A |
Approximately 1–40 mm for common production work; piercing capacity is lower than severance capacity |
Approximately ±0.15–0.50 mm, depending on torch, table, and material |
Lower purchase cost, high productivity on carbon steel, and effective thick-plate cutting |
Wider kerf and larger heat-affected zone than laser; produces dross and fumes |
US$25,000–120,000 |
Replace electrodes and nozzles, drain the air system, clean the slats, remove dross, inspect torch height control |
Air quality, fume extraction or water table, torch consumable cost, automatic height sensing, CNC compatibility |
| 5 |
CNC Waterjet Cutter |
Heat-sensitive materials, thick plate, stone, glass, composites, and mixed materials |
1,500 × 3,000 mm to 2,000 × 6,000 mm |
30–100 hp pump |
Approximately 1–150 mm, depending on material and required edge quality |
Approximately ±0.10–0.25 mm |
No heat-affected zone, broad material compatibility, and excellent performance on thick materials |
Slower than laser for thin sheet; high water, abrasive, pump, and waste-management costs |
US$100,000–300,000+ |
Replace orifice and focusing tube, inspect high-pressure seals, manage abrasive, clean the tank and filtration system |
Water treatment, drainage, abrasive disposal, pump service network, noise control, required edge quality |
| 6 |
CNC Guillotine Shear |
Straight-line blanking of repetitive sheet-metal batches |
1,000–4,000 mm cutting length |
Mechanical or hydraulic; commonly 4–30 kW |
Approximately 0.5–16 mm mild steel, depending on cutting length and machine design |
Approximately ±0.05–0.15 mm back-gauge positioning |
Fast, simple, economical, and productive for straight cuts with minimal programming |
Cannot produce internal profiles, holes, or complex contours; generates more scrap in nested work |
US$20,000–100,000 |
Maintain blade clearance, sharpen or replace blades, lubricate guides, inspect hydraulic oil and back gauge |
Cutting length, maximum thickness, blade material, back-gauge travel, hold-down system, safety guarding |
| 7 |
CNC Turret Punch Press |
High-volume punching, louvers, perforations, forming, and repetitive holes |
1,250 × 2,500 mm to 1,500 × 4,000 mm |
20–40 tons punching force |
Typically up to 6 mm mild steel, with capacity varying by material and tool size |
Approximately ±0.05–0.10 mm positioning accuracy |
Excellent for repeated holes, forming operations, and low-to-medium complexity profiles |
Tooling marks, noise, and limitations on thick material or highly intricate contours |
US$80,000–250,000 |
Inspect and sharpen punches and dies, maintain tool clearance, lubricate the turret, remove slugs |
Tool station count, auto-indexing, forming height, sheet handling, tooling availability, software integration |
| 8 |
Laser-Punch Combination Machine |
Complex parts requiring both contour cutting and punching or forming |
1,250 × 2,500 mm to 1,500 × 3,000 mm |
Laser: approximately 2–4 kW; punching: approximately 20–30 tons |
Typically up to 6–8 mm mild steel, depending on the integrated configuration |
Approximately ±0.05–0.10 mm |
Combines two processes, reduces handling, and supports complex parts with fewer setups |
High purchase cost and more complex service requirements; may be inefficient for single-process jobs |
US$180,000–450,000+ |
Maintain laser optics and chiller, service punching tools, inspect alignment, clean scrap and slugs |
Process mix, automation, tool library, software workflow, material handling, service coverage, floor space |
| 9 |
Tube and Profile Laser Cutter |
Frames, furniture, automotive components, handrails, and structural profiles |
Tube length: 3,000–6,500 mm; round tube diameter: approximately 20–230 mm |
1.5–6 kW |
Approximately 0.8–20 mm wall thickness, depending on material and tube geometry |
Approximately ±0.05–0.15 mm |
Automates cutting, drilling, and slotting on round, square, rectangular, and selected open profiles |
Requires accurate tube loading and profile data; less suitable for flat-sheet-only production |
US$100,000–300,000 |
Clean chuck and support rollers, inspect clamping, maintain optics and chiller, verify tube alignment |
Maximum tube size, automatic loading, chuck design, profile library, remnant management, collision protection |
| 10 |
Portable CNC Oxy-Fuel Cutter |
Very thick carbon-steel plate, field work, repair, and large structural components |
Rail length commonly 2,000–12,000 mm or more |
Low electrical load; uses oxygen and fuel gas |
Approximately 6–300 mm carbon steel, depending on torch and gas configuration |
Approximately ±0.5–1.5 mm |
Low equipment cost, portable operation, and effective cutting of very thick mild steel |
Slow on thin sheet; limited to oxidizable metals and produces a larger heat-affected zone |
US$8,000–60,000 |
Inspect hoses and regulators, clean torch tips, check gas leaks, maintain rails and flame-arrestor systems |
Gas-safety certification, torch capacity, rail straightness, flame-failure protection, operator training, ventilation |